China has become a major sourcing base for industrial casting equipment, but choosing the right supplier requires more than comparing prices. A reliable Tin Bar Casting Machine should produce consistent bar dimensions, stable alloy quality, and clean surfaces during continuous operation. Buyers must examine furnace design, casting speed, cooling control, mold durability, electrical safety, and after-sales support.
Li Wei, a senior tin-processing equipment engineer with practical factory experience, says, “A good casting machine is judged by stable output after many production cycles, not by its first successful bar.” That point matters. A polished sample can hide uneven cooling, metal loss, or frequent mold replacement. Real performance appears beside the furnace, where operators monitor temperature readings, molten tin flow, and the sound of the cooling system.
The best China manufacturer should provide more than a catalog and a confident sales promise. It should explain installation conditions, energy use, maintenance intervals, and realistic production capacity. Factory testing, material certificates, clear drawings, and responsive technical service strengthen trust. Yet no machine is perfect. Even an efficient Tin Bar Casting Machine may need adjustment when alloy composition, workshop temperature, or operator habits change.
This guide examines how to evaluate Chinese suppliers through engineering details, production evidence, customization ability, and service reliability. The goal is practical judgment. Not easy marketing claims. A careful buyer should ask difficult questions before signing an order, because dependable casting begins long before the machine reaches the workshop.
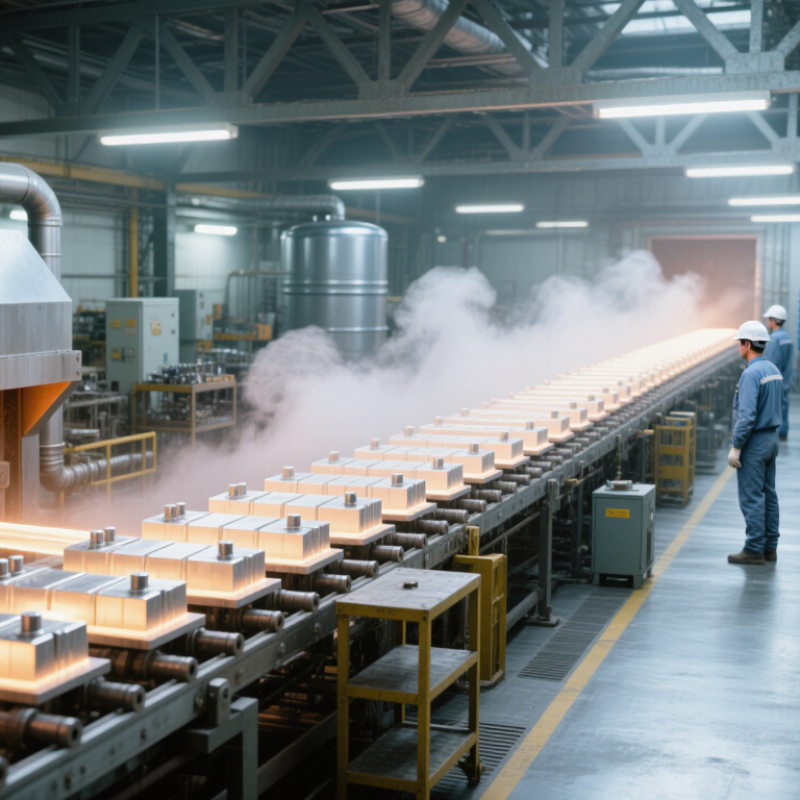
A tin bar casting machine is industrial equipment that melts tin, controls its temperature, and forms it into solid bars. The process usually includes a melting furnace, transfer channel, casting mold, cooling section, and cutting unit. In simple terms, it turns liquid tin into measured, stackable products.
The International Tin Association estimated that solder accounted for about 48% of global tin use in 2023. This demand requires stable bar chemistry and repeatable dimensions. The U.S. Geological Survey reported approximately 290,000 metric tons of global tin mine production in 2023. Such limited supply makes recovery rate important. A small amount of metal loss can affect production costs.
Good equipment should maintain steady pouring, even cooling, and clean mold release. Operators should check furnace temperature, bar weight, surface cracks, and slag levels during every shift. Practical testing matters more than catalog claims. A machine may reach its rated capacity, yet produce uneven bars under real conditions. That weakness is easy to overlook. Energy use, maintenance access, and operator safety also deserve careful measurement. The International Organization for Standardization encourages documented quality controls, but each casting line still needs process-specific validation. I would not judge a machine by output alone. Consistency is the harder target.
A tin bar casting machine converts measured molten tin into uniform solid bars. The process begins with an electrically heated melting chamber. Operators monitor temperature with a calibrated sensor. The metal must flow smoothly without excessive oxidation. A controlled outlet sends molten tin into metal molds. Mold dimensions determine each bar’s width, length, and weight. Small temperature changes can affect surface finish. This is where practical experience matters.
As the molds move through the cooling section, water jackets or forced air remove heat. The tin solidifies from the mold walls toward the center. A steady cooling rate helps prevent dents, cracks, and internal shrinkage. After solidification, an automatic ejector releases each bar onto a conveyor. Sensors may check presence, dimensions, and temperature. Manual sample weighing remains useful because automation can miss unusual defects.
The operator inspects edges, color, and surface smoothness before packing. Clean molds are essential. Residue can create drag marks or trapped particles. In real production, the first cast is not always perfect. Settings may need adjustment after observing flow and cooling behavior. Those changes should be recorded and verified against quality requirements. Proper guarding, ventilation, and heat-resistant procedures protect workers near the machine.
| Process / Machine Dimension | Typical Value or Range | How It Works | Key Factors Affecting Performance |
|---|---|---|---|
| Raw Material | Pure tin, tin-lead solder, or lead-free tin alloy | Certified ingots, granules, or recycled tin feedstock are loaded into the melting chamber. | Alloy composition, cleanliness, moisture, oxidation, and incoming material size. |
| Tin Melting Point | Pure tin: approximately 231.9°C | The heating system raises the charge above its melting point until a uniform liquid bath is formed. | Different solder alloys have different melting and solidification ranges. |
| Recommended Holding Temperature | Typically 260–340°C for tin-based casting | A controlled temperature margin keeps the metal fluid while limiting unnecessary overheating and oxidation. | Alloy type, bar thickness, mold speed, pouring method, and required surface quality. |
| Heating System | Electric resistance or induction heating | Electrical energy heats the crucible or melting tank; a controller regulates the set temperature. | Heating power, insulation, temperature sensor position, and thermal uniformity. |
| Melting Capacity | Approximately 30–500 kg per batch | The charge is melted in a crucible or tank sized for the required production volume. | Furnace volume, heating power, charge density, alloy, and melting cycle time. |
| Metal Transfer | Gravity pouring or metered pump transfer | Molten tin flows from the holding area into individual molds or a continuous casting channel. | Flow rate, head pressure, transfer temperature, dross control, and turbulence. |
| Casting Method | Permanent mold, chain mold, or continuous strand casting | The mold defines the bar profile while the metal solidifies under controlled cooling. | Mold material, mold geometry, release treatment, cooling rate, and line speed. |
| Typical Bar Cross-Section | Commonly 10 × 10 mm to 50 × 50 mm | Interchangeable molds or adjustable tooling produce the required bar dimensions. | Product specification, shrinkage allowance, mold wear, and dimensional tolerance. |
| Cooling System | Air cooling or water-cooled mold channels | Heat is removed from the mold and solidifying bar to stabilize the shape before discharge. | Cooling-water flow, inlet temperature, mold thermal conductivity, and casting speed. |
| Production Rate | Approximately 50–500 kg per hour | The line combines melting, filling, solidification, demolding, and collection into a repeatable cycle. | Bar size, alloy, number of mold cavities, cycle time, and operator loading method. |
| Temperature Control Accuracy | Commonly within approximately ±2–5°C | Thermocouples or resistance temperature detectors provide feedback to the controller. | Sensor calibration, controller quality, heating response, and insulation condition. |
| Demolding and Discharge | Manual, pneumatic, hydraulic, or servo-assisted | Solidified bars are released from the mold and transferred to a conveyor, bin, or cutting station. | Release angle, bar temperature, mold coating, extraction timing, and automation level. |
| Bar Length Control | Fixed mold length or approximately 100–1,000 mm continuous cut length | A mold cavity or synchronized cutting unit determines the finished bar length. | Encoder accuracy, cutting speed, product temperature, and dimensional requirements. |
| Control System | Temperature controller with optional PLC and touchscreen HMI | The system monitors temperature, conveyor speed, filling sequence, alarms, and safety interlocks. | Automation scope, sensor reliability, recipe management, and operator training. |
| Common Quality Checks | Weight, dimensions, surface condition, composition, and internal defects | Finished bars are inspected to confirm consistent geometry and alloy conformity. | Sampling frequency, laboratory equipment, casting stability, and material traceability. |
Note: The values shown are typical engineering ranges for tin-based bar casting equipment. Actual specifications depend on the alloy, bar dimensions, required output, mold design, and level of automation.
China Top Tin Bar Casting Machine Manufacturer?
China-made tin bar casting machines increasingly focus on stable temperature control, repeatable molds, and practical automation. The USGS Mineral Commodity Summaries 2025 estimated global tin mine production at about 290,000 metric tons in 2024. This limited supply makes metal recovery and casting consistency financially important. A reliable machine should use closed-loop temperature monitoring, usually through thermocouples and programmable controllers. Operators can then maintain a narrow pouring range and reduce oxidation, dross, and uneven bar surfaces.
Key Features of China-Made Tin Bar Casting Machines
Many modern systems combine electric or induction melting with automatic bar molds, water cooling, and conveyor discharge. Water flow sensors help protect molds from overheating. Adjustable mold sizes support different weights, from small ingots to larger industrial bars. Some lines also include weighing systems and batch records, which improve traceability during inspection. The International Tin Association continues to identify electronics, solder, and chemical applications as major tin demand sectors. That makes dimensional accuracy more than a visual issue.
Small details matter.
In practical factory testing, the machine should be checked with the actual tin grade, mold material, and production speed. A specification sheet alone cannot reveal cooling fluctuations or difficult cleaning points. Energy consumption also deserves attention; a cheaper furnace may require more electricity during repeated heating cycles. No casting line is perfect. Operators still need training, preventive maintenance, and sensible control limits. Those human factors are often overlooked, even when the equipment itself appears technically advanced.
China Top Tin Bar Casting Machine Manufacturer?
How to Evaluate a Chinese Tin Bar Casting Machine Manufacturer
A reliable evaluation starts with production evidence, not a polished website. The USGS Mineral Commodity Summaries 2025 estimated global tin mine production at about 290,000 metric tons in 2024. This scale makes process consistency important, especially when buyers need stable bar weight, surface quality, and low metal loss. Ask the manufacturer for recent machine videos, factory records, and customer references from comparable output levels.
Check the casting line in detail. Measure temperature control near tin’s 231.9°C melting point. Review furnace insulation, mold material, cooling speed, conveyor alignment, and automatic bar counting. Request test results for weight tolerance, cycle time, energy use, and rejected bars. Numbers expose weak promises. A serious supplier should explain calibration methods and spare-part availability. Confirm whether the quoted capacity means theoretical output or tested production.
Audit quality systems, worker training, and export experience. Request material certificates for molds and electrical components, plus an inspection report before shipment. The International Tin Association identifies solder, chemicals, and tinplate among major tin-use sectors; each may require different bar specifications. Do not judge only by price. The cheapest quote can be the most expensive lesson. I would still challenge every claimed number, because one factory trial cannot represent a full year of production. Demand evidence.
A reliable manufacturer should demonstrate stable heating and temperature control across the alloy range used in production. The chart shows published melting ranges for common tin materials and provides a practical reference for reviewing furnace capacity, temperature accuracy, casting stability, and factory acceptance test results.
Tin bar casting equipment supports solder production, metal refining, electroplating supply, and controlled alloy preparation. Each application demands different casting speed, bar dimensions, and cooling performance. A workshop producing narrow solder bars may need a compact continuous caster with precise temperature control. Larger operations often require automated pouring, water circulation, and synchronized cutting. Clean surfaces matter. Oxide layers can weaken later processing.
Selection should begin with material requirements, not machine appearance. Confirm the tin grade, alloy composition, melting range, and expected hourly output. The mold must match the required bar size and surface finish. Stable heating reduces temperature swings and protects alloy consistency. Check whether the system records temperature, batch numbers, and production speed. These records support quality control and practical traceability.
Safety and maintenance deserve equal attention. Look for insulated surfaces, emergency stops, guarded moving parts, and accessible cleaning points. Ask for test data using a similar alloy, not only standard samples. A supplier with engineering documentation, operator training, and spare-part guidance is easier to trust. In real production, the fastest machine is not always the best choice. I have seen output targets expose cooling limits and produce uneven bars. That mistake is expensive, but it reveals a useful lesson: selection should follow stable quality, energy use, and service access. Some specifications will still need revision after installation.
Copyright ©2024 Elephant Lifting Products | All rights reserved.
38381 N Robert Wilson Rd, Gonzales, LA 70737 USA
Toll Free: (888) 844-6113 | Phone: (225) 644-6113 | Fax: (225) 644-6695
Email: sale@floralift.org