Language:

How to Choose the Right Custom Titanium Plate?

Choosing the right Custom Titanium Plate begins with understanding its real working environment. Load, temperature, corrosion, weight, and installation space all matter. A plate used in aerospace equipment may need different properties from one used in medical or industrial assemblies. The correct choice is never based on appearance alone.

Materials engineer Matthew J. Donachie Jr. offered a practical reminder: “Material selection must begin with service requirements.” That principle remains useful today. Grade 2 titanium may suit applications requiring strong corrosion resistance and easier forming. Grade 5 titanium can provide higher strength, but machining may demand more control. Small details matter. Hole spacing. Edge radius. Surface finish. Plate thickness.

A reliable supplier should review drawings, tolerances, loading conditions, and inspection requirements before production. Ask for material certificates, dimensional reports, and traceability records. Check whether the manufacturer understands heat treatment, CNC machining, deburring, and surface protection. A clean edge can prevent assembly problems. A poorly positioned hole cannot.

There is no universally perfect Custom Titanium Plate. That is easy to forget. Designers sometimes focus on strength and overlook fatigue, galvanic corrosion, or installation access. Even experienced teams can miss a constraint during early planning. A short design review can expose those weaknesses. It may also reduce wasted material and costly rework.

The best decision balances performance, manufacturability, compliance, lead time, and total cost. Choose evidence over attractive promises. Ask precise questions. Then verify the answers.
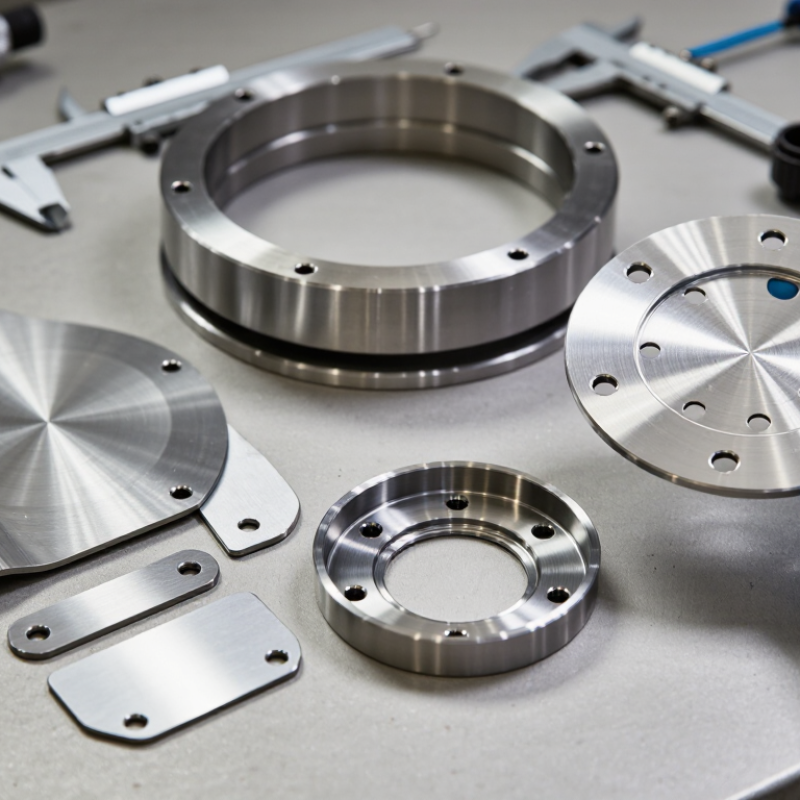
How to Choose the Right Custom Titanium Plate?

Define the Application and Performance Requirements

How to Choose the Right Custom Titanium Plate?

Defining the application comes before choosing a titanium plate. A plate for a lightweight bracket may need different properties than one exposed to seawater. Identify the load, operating temperature, contact materials, and expected service life. Consider static stress, vibration, fatigue, and possible impact. Small details matter. A 2 mm thickness change can affect stiffness, weight, and machining cost. In practical design reviews, engineers should also confirm dimensions, tolerances, surface finish, and joining methods. A technically strong design can still fail if it cannot be manufactured consistently.

Tips: Write the working conditions clearly. Include maximum load, temperature range, chemical exposure, and cleaning methods. Ask for material certificates and inspection records. Verify the supplier’s testing process, traceability, and ability to meet the required tolerance. Do not select a grade from a table alone. Testing may reveal unexpected distortion or surface damage.

Performance requirements should match the real environment, not an ideal laboratory setting. For example, a plate used near saltwater may require careful corrosion evaluation. A plate facing repeated cycles needs fatigue data, not only tensile strength. Thermal expansion may also affect bolts, seals, and nearby components. One common mistake is choosing the strongest option without checking machinability or cost. That choice may look safe, but it can create delays. A better approach combines engineering calculations, prototype inspection, and documented quality checks. Reconsider assumptions when test results disagree with the original design.
Select the Titanium Grade and Material Specifications

Selecting the titanium grade is the core decision in a custom plate project. Grade 2 commercially pure titanium offers strong corrosion resistance, good formability, and easier machining. ASTM B265-24 lists a minimum tensile strength of about 345 MPa for Grade 2 plate. It suits chemical equipment, heat exchangers, and marine parts. Grade 5, or Ti-6Al-4V, reaches about 895 MPa minimum tensile strength under the same standard. It is stronger, but less ductile and usually harder to machine.

Material specifications must match the real load, temperature, and environment. For medical or low-temperature applications, Grade 23 ELI may be preferable because its reduced interstitial content improves fracture toughness. Aerospace specifications often require tighter chemistry, ultrasonic inspection, and traceable heat numbers. ASTM B265 defines requirements for titanium and titanium-alloy sheet and plate, while ASM Handbook data shows that heat treatment can change strength and ductility considerably. Do not select Grade 5 only because it sounds stronger. That choice can increase cost and create unnecessary machining problems.

Tip: Request the alloy grade, thickness tolerance, surface condition, test certificate, and heat number before production. Confirm whether the plate needs annealing, stress relief, or ultrasonic testing. A small detail matters here. I have seen designs focus on tensile strength while ignoring plate flatness and residual stress. That mistake can appear later, during forming or welding. Always review the final specification with a qualified materials engineer.

Determine the Plate Dimensions, Tolerances, and Surface Finish

How to Choose the Right Custom Titanium Plate?

When choosing a custom titanium plate, start with the load, not the catalog. Define length, width, thickness, holes, edge profiles, and bend lines. A 0.5 mm thickness error can affect stiffness, weight, and assembly fit. However, the acceptable error depends on the application, not personal preference. ASTM B265 covers titanium plate, sheet, and strip requirements.

The U.S. Geological Survey’s Mineral Commodity Summaries 2024 estimated global sponge titanium production at about 280,000 metric tons in 2023. This supply scale does not remove variation in lead times or available sizes. Request a certified mill test report. Specify the grade, nominal dimensions, tolerance class, flatness, and inspection method. Use ASME Y14.5 when hole location, parallelism, or profile controls are important. Surface finish also needs a measurable target. For a machined mating face, state a value such as Ra 1.6 μm and identify the measurement standard. A “smooth finish” is too vague.

Tips: Send a dimensioned drawing and a functional sample. Separate critical surfaces from cosmetic ones. Request flatness data across the full plate. Do not accept “tight tolerance” without numbers. Over-specifying every surface can increase cost without improving performance. A controlled mill finish may work better than a mirror finish in some assemblies. Still, the first specification may be wrong after forming. Recheck it.

How to Choose the Right Custom Titanium Plate? - Determine the Plate Dimensions, Tolerances, and Surface Finish

Selection Factor Recommended Specification Typical Custom Range Tolerance / Control Target Suitable Surface Finish When to Choose It
Titanium Grade 2 Commercially pure titanium with excellent corrosion resistance Thickness: 0.5–100 mm
Width: up to 2,000 mm
Length: up to 6,000 mm
Thickness: typically ±0.10 mm for thin plate and tighter by agreement for machined plate
Flatness: commonly controlled to approximately 3–6 mm per metre
Hot-rolled, pickled, or ground; approximately Ra 1.6–6.3 µm depending on processing Good for chemical-processing equipment, heat exchangers, marine components, and applications requiring high corrosion resistance rather than maximum strength.
Titanium Grade 5 Ti-6Al-4V alloy for high strength-to-weight performance Thickness: 0.5–150 mm
Width: up to 2,000 mm
Length: up to 6,000 mm
Thickness: typically ±0.10–0.25 mm for rolled plate, depending on thickness and specification
Flatness: commonly controlled to approximately 3–6 mm per metre
Mill finish, pickled, bead-blasted, ground, or machined; approximately Ra 0.8–6.3 µm Suitable for aerospace structures, medical components, marine hardware, and demanding parts where strength and low density are important.
Titanium Grade 23 Extra-low-interstitial Ti-6Al-4V alloy for improved fracture toughness and biocompatibility Thickness: 0.5–100 mm
Width: up to 1,500 mm
Length: up to 4,000 mm
Thickness: typically ±0.10–0.25 mm, subject to the ordered thickness and applicable material specification
Flatness: commonly controlled to approximately 3–5 mm per metre
Fine-ground or polished; approximately Ra 0.4–1.6 µm for critical contact surfaces Recommended for orthopedic, dental, and other high-performance applications requiring enhanced toughness and a clean, controlled surface.
Plate Thickness Select the minimum thickness that meets structural, thermal, and machining requirements Thin plate: 0.5–6 mm
Medium plate: 6–25 mm
Heavy plate: above 25 mm
Use a general rolled-plate tolerance for non-critical parts; specify a tighter custom tolerance only where fit, sealing, or machining allowance requires it. Thin material is often supplied cold-rolled or ground; thicker material is commonly hot-rolled and pickled. Choose thin plate to reduce weight, medium plate for general fabricated parts, and heavy plate for load-bearing or extensively machined components.
Plate Width and Length Define finished dimensions plus cutting and machining allowance Common custom sizes: 300–2,000 mm wide × 500–6,000 mm long Cutting tolerance is often approximately ±1–3 mm; precision sawing or machining can achieve tighter dimensional control by agreement. Specify the final finish after cutting if the edges or faces will remain visible or functional. Use near-net dimensions to reduce material waste, but include sufficient allowance for trimming, distortion removal, and final machining.
General Machined Surface Standard CNC-milled or turned surface for non-sealing faces Typical roughness: Ra 1.6–3.2 µm Dimensional tolerance commonly ±0.05–0.15 mm, depending on geometry, size, and inspection method Uniform tool-marked finish with deburred edges Use for brackets, covers, structural plates, and parts where appearance is important but fluid sealing is not required.
Fine Ground Surface Controlled, uniform finish for contact and appearance Typical roughness: Ra 0.8–1.6 µm Flatness and parallelism should be stated separately; a practical target is 0.05–0.20 mm over the specified inspection length. Fine-ground, satin, and low-reflection appearance Choose this finish for sliding interfaces, assembly contact faces, and components requiring more consistent surface texture.
Polished Surface Low-roughness surface for appearance or hygiene-sensitive applications Typical roughness: Ra 0.2–0.8 µm Specify allowable scratches, pits, waviness, and inspection lighting in the drawing or purchase specification. Bright or satin polish, depending on abrasive sequence Recommended for medical, laboratory, architectural, and clean-service components where smoothness and visual quality are critical.
Edge Condition Deburred, chamfered, or radiused edges Typical chamfer: 0.2–1.0 mm
Typical edge radius: 0.5–2.0 mm
Edge-break tolerance should be stated when the plate is used for assembly, sealing, or handling-sensitive equipment. Match the edge finish to the adjacent plate surface to prevent sharp transitions. Specify edge treatment to improve safety, prevent stress concentration, and ensure reliable fit during assembly.
Inspection Requirements Document grade, dimensions, tolerances, flatness, roughness, and test requirements Dimensional inspection, visual inspection, surface-roughness measurement, and material certificate For critical parts, add chemical composition, mechanical properties, ultrasonic testing, and traceability requirements. Inspect the surface after the final finishing operation, not only after initial rolling. Use enhanced inspection for aerospace, medical, pressure-containing, fatigue-critical, or safety-related components.

Note: The values shown are typical engineering planning ranges. Final dimensions, tolerances, surface roughness, testing, and acceptance criteria should be confirmed against the applicable material standard and the part drawing.

Evaluate Manufacturing Methods and Customization Options

How to Choose the Right Custom Titanium Plate?

Choosing a custom titanium plate starts with the manufacturing method. CNC machining suits plates requiring precise pockets, countersinks, or narrow tolerances. Laser cutting works well for clean profiles and repeated openings, while waterjet cutting reduces heat exposure near delicate edges. Rolled plate is practical for larger panels and consistent thickness. Additive manufacturing may solve complex shapes, but it can increase cost and require extra finishing.

Customization should match the part’s actual working conditions. Specify the titanium grade, thickness, surface finish, hole pattern, edge radius, and dimensional tolerance. For example, a 6 mm plate with four 10 mm holes needs different inspection controls than a thin cover with simple slots. Ask for material certificates, inspection records, and traceability from raw stock to final part. These details support reliability. They also reveal weak quality control.

Tips: Request a drawing review before production. Confirm whether measurements use millimeters. Ask how distortion will be checked after cutting. A low quote may look attractive, but it can hide secondary machining or poor surface preparation. I would not choose a supplier based on price alone. Still, even experienced buyers sometimes over-specify tolerances that the assembly does not need. That mistake adds cost without improving performance. Share photographs, load information, and a sample dimension whenever possible. Clear input usually produces a more dependable custom plate.

Verify Quality Standards, Testing, and Supplier Capabilities

Choosing the right custom titanium plate starts with verifiable quality standards. ASTM B265 defines requirements for titanium and titanium alloy plate, including grades, dimensions, and mechanical properties. Ask for the exact grade, heat number, thickness tolerance, and applicable standard before approving a quotation. A certificate alone is not enough. The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates worldwide, yet certification does not prove every batch meets your technical needs.

Request complete test reports linked to the same heat number. Tensile strength and elongation should follow ASTM E8/E8M, while chemical composition requires calibrated laboratory analysis. Ultrasonic inspection can reveal internal discontinuities that remain invisible on a polished surface. Review sampling frequency, acceptance limits, equipment calibration, and laboratory accreditation. Small gaps matter.

Supplier capability deserves equal attention. Check whether the supplier controls forging, rolling, heat treatment, machining, surface finishing, and final inspection internally. Traceability should follow the plate from melting through shipment. Ask for nonconformance records and corrective-action examples. This may feel intrusive, but vague answers are a warning. In practice, even a technically strong supplier can miss a delivery detail, so drawings, inspection plans, and revision control must be confirmed in writing.

Member of

Associated Wire Rope FabricatorsMHI MemberNetPlus Alliance Member Steel Erectors Assocation STADFA member

Terms of Sale | Privacy Policy