Language:

7 Tips for Choosing Carbon Black Masterbatch

A black plastic part can hide a complicated materials decision. Carbon Black Masterbatch influences colour, UV protection, conductivity, and processing behavior. The right grade depends on the application, not just the deepest shade. Small details matter.

PlasticsEurope’s 2024 report, Plastics – the Fast Facts, estimates global plastics production at 413.8 million tonnes in 2023. This figure does not measure masterbatch demand, but it illustrates the scale of products that depend on consistent polymer performance. For manufacturers, a poor match can show up as streaks across a molded panel, unstable extrusion, or added wear on processing equipment. Even experienced teams get this wrong.

Choosing a grade means checking carbon black loading, dispersion quality, carrier compatibility, and the end product’s requirements. Particle characteristics matter, too. A formulation suited to outdoor pipe may not fit thin packaging film or conductive components. Not always. Supplier data can help, but test results should reflect your own resin, equipment, and processing conditions. Ask for technical documentation, batch consistency information, and application-specific guidance. Then verify performance with a controlled trial. These seven tips outline practical checks for comparing grades and asking better supplier questions. No single specification tells the whole story. A little doubt is useful.
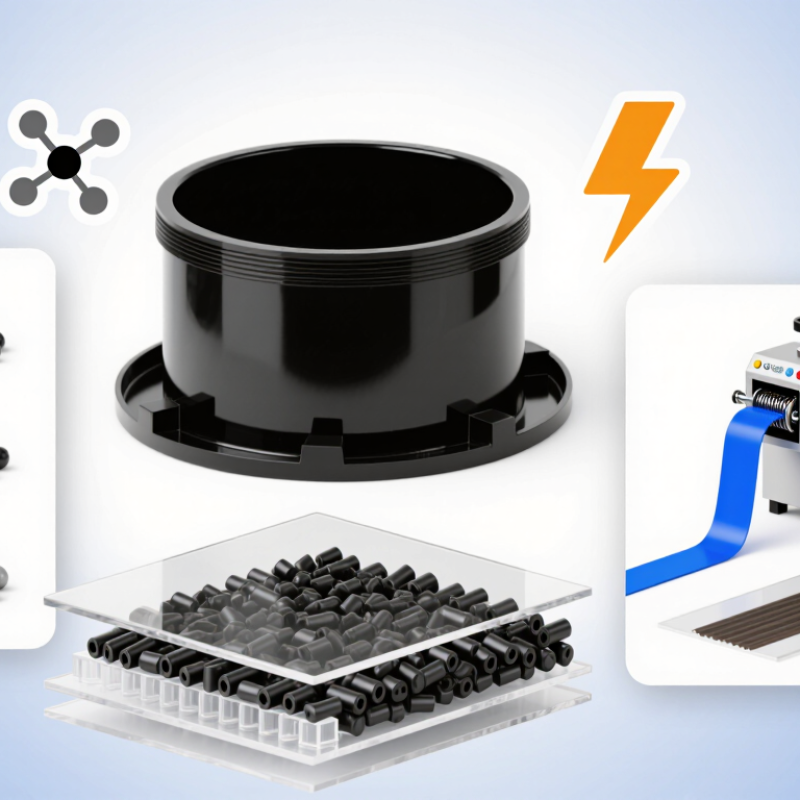
7 Tips for Choosing Carbon Black Masterbatch

Define the Application and Performance Requirements

Before comparing carbon black masterbatch grades, define the finished part and its working conditions. A black outdoor pipe needs weathering resistance and consistent dispersion; an electrical component may need a controlled resistivity range. A film producer may care more about jetness, thin-section coverage, and screen-pack pressure. Specify the polymer, let-down ratio, processing temperature, and target tests. Small details matter. A grade that performs well in HDPE extrusion may behave differently in a polypropylene molded part.

PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. That scale spans very different polymers and processes, so one generic “blackness” target is not enough. The International Carbon Black Association describes carbon black’s roles in rubber and plastics, including pigmentation and UV protection; the required balance depends on the end use. Set measurable limits for color strength, dispersion, melt flow, and—where relevant—weathering or electrical resistance. Test samples in the actual resin and on the intended line. A plaque may look excellent, yet thin film can reveal specks or uneven shade. I’ve seen specifications overlook this. Recheck them.
Compare Carbon Black Content and Dispersion Quality

Tip 1: Compare carbon black content by checking the technical data sheet and confirming the test method. A higher percentage can improve color strength or UV protection, but it may also increase viscosity and make processing harder. Compare grades at the same loading; otherwise, the numbers can mislead.

Tip 2: Ask for dispersion results, not just a statement that dispersion is “good.” Examine a molded plaque or film for specks, streaks, and uneven shade. A microscope-based rating can help, but results depend on the sample and method. Small details matter. If possible, run the same trial conditions for each candidate.

Tip 3: Judge content and dispersion together. Poorly dispersed carbon black may create visible defects even when the total content looks suitable. Request a sample and record screw speed, melt temperature, and let-down ratio during a trial. Then compare color uniformity and surface finish. Check both. One practical caveat: lab plaques may look better than parts made on a busy production line, so verify performance at your actual processing scale.

Check Carrier Resin Compatibility and Processing Needs

Carrier resin compatibility is more than matching “PE” or “PP” on a datasheet. Check the exact polymer grade, melt-flow behavior, and processing temperature. A carrier that softens too early can cause unstable feeding; one that flows poorly may leave streaks or black specks. Compare melt-flow data only when test conditions match. One awkward truth: a paper match can still disappoint on the production line.

Tip: Trial the masterbatch in your actual resin at the intended letdown ratio. Run it through the normal screw, temperature profile, and output rate. Watch for pressure changes, die build-up, uneven color, or rough surfaces. Record results, even if the first trial looks acceptable. The Plastics Europe report Plastics – the Fast Facts 2024 estimates global plastics production at 413.8 million tonnes in 2023. That figure is not a masterbatch-performance measure, but it shows why small process losses matter at scale.

Ask the supplier for carrier details and application-specific processing guidance, then verify them with a controlled trial. Keep a molded plaque or film sample as a visual reference. If the masterbatch disperses well but changes impact strength or surface feel, revisit the carrier choice—not just the pigment loading. A quick line test helps, but it is not a substitute for checking the finished part.

Assess Color, UV Protection, and Mechanical Performance

A carbon black masterbatch should be judged by the finished part, not by pellet color alone. A deep, even black can hide poor dispersion. Check molded plaques for streaks, specks, and shade variation, then compare samples at the same let-down ratio. Small differences become obvious on a glossy surface. They can also signal agglomerates that weaken local areas.

UV protection depends on loading and dispersion. ISO 4427-2:2019 specifies 2.0–2.5% carbon black by mass for black polyethylene pressure pipes, with dispersion requirements. ISO 6964 provides a method for measuring carbon black content, while ISO 18553 evaluates dispersion. These are useful benchmarks, not a guarantee that every formulation will perform alike. Ask for test results on the intended resin and part thickness. A higher loading is not automatically better.

Mechanical checks matter too. Compare tensile strength, elongation, and impact results against an unpigmented control, using consistent processing conditions. ISO 527 and ISO 179 describe common tensile and impact test methods. Watch for brittle edges, reduced elongation, or unstable extrusion pressure. A slightly duller plaque may still be the better choice if it disperses cleanly and retains impact strength. I would not select on color alone.

7 Tips for Choosing Carbon Black Masterbatch - Assess Color, UV Protection, and Mechanical Performance

Tip What to assess Useful data or screening guidance How to verify
1. Define the color target Blackness, undertone, gloss, and consistency at the intended let-down ratio and part thickness. Compare molded or extruded samples with an approved control. Record CIELAB L*, a*, and b* values; lower L* generally indicates a darker appearance. Measure color under consistent lighting, surface finish, and specimen thickness. Set an application-specific ΔE tolerance rather than relying on visual judgment alone.
2. Check carbon black content The masterbatch loading and the resulting carbon black concentration in the finished product. Commercial masterbatch formulations commonly use a broad range of carbon black loadings, often about 20–50% by weight. The required final concentration depends on polymer, product geometry, and performance requirements. Confirm the supplier’s declared content and calculate the final loading from the let-down ratio. Use an appropriate recognized carbon-black-content method for the polymer and application.
3. Evaluate UV protection Carbon black type, dispersion, final loading, product thickness, and the outdoor exposure conditions. For some polyethylene geomembrane specifications, 2–3% carbon black in the finished compound is commonly used; this is not a universal target for other products or polymers. Test representative finished parts using an agreed weathering protocol, such as fluorescent UV exposure, and assess property retention against the product specification.
4. Inspect dispersion quality Agglomerates, streaks, specks, and variation across the molded or extruded part. Good dispersion supports more uniform color and UV performance. There is no single visual or numerical acceptance limit suitable for every end use. Review thin sections or plaques under consistent conditions and, where needed, use a documented microscopic dispersion rating method appropriate to the polymer.
5. Match the carrier resin Compatibility with the base polymer, processing temperature, and molding or extrusion process. A compatible carrier can help reduce processing issues and property changes. Check whether the carrier is suitable for the resin family and any food-contact or regulatory requirements. Run a production-representative trial and check for surface defects, plate-out, odor, and changes in part appearance or processing stability.
6. Compare melt flow and processability Melt flow rate (MFR), feeding behavior, pressure, and output at the intended processing conditions. MFR values are meaningful only when the test temperature and load are stated. Compare the masterbatch and finished blend with the process requirements, not with an unrelated resin grade. Check MFR using the same test conditions, such as those specified in ASTM D1238, then validate on the actual equipment.
7. Confirm mechanical-property retention Tensile strength, elongation, impact resistance, and any other properties critical to the part. Results depend on the base resin, carbon black loading, dispersion, and processing history. Establish acceptance limits from the product specification or a qualified control formulation. Test representative specimens using consistent preparation and methods, such as ASTM D638 for tensile properties, and compare results with the agreed baseline.

Screening values are application-dependent; confirm the final formulation and acceptance criteria through supplier documentation and testing of production-representative parts.

Verify Quality Controls and Supplier Reliability

When evaluating carbon black masterbatch, ask for batch-specific certificates of analysis, not a generic product sheet. Check carbon black content, moisture, ash, and dispersion against agreed limits. For tint strength, ASTM D3265 provides a standardized test method. Request the test method, result, and sample identification; a number without traceability is weak evidence. Ask the supplier to retain samples and explain how it handles out-of-specification batches. Ask for evidence.

Supplier systems matter, but certificates are only a starting point. The ISO Survey 2022 recorded 1,265,216 valid ISO 9001 certificates worldwide. That figure shows how common certification is; it does not prove consistent masterbatch quality or dependable delivery. Review the supplier’s change-control process, complaint records, and documented delivery performance. Ask how quickly it reports production changes or raw-material shortages. OECD’s Global Plastics Outlook (2022) reported 460 million tonnes of plastics produced in 2019, twice the 2000 level. In a large, variable supply chain, small batch differences can show up as streaks or uneven blackness in molded parts. A polished audit file can still miss problems on the line. Compare trial batches under your own processing conditions, and record the results before approving routine orders.

Member of

Associated Wire Rope FabricatorsMHI MemberNetPlus Alliance Member Steel Erectors Assocation STADFA member

Terms of Sale | Privacy Policy